

Industrial Bearing Quality Control & ISO 9001 Metrology Assurance
Quality in heavy-duty rolling bearings cannot be inspected in after final grinding—it is engineered into every melt check, heat-treatment cycle, raceway profile, and assembly clearance gate. Backed by ISO 9001 and ISO 14001 management systems across our Wafangdian manufacturing hub, ZQM executes disciplined, traceable inspection from raw steel to export crating.
Process-Built Reliability & Four-No Quality Discipline
End-of-line screening catches defects too late. ZQM enforces preventive statistical and metallurgical controls at every turning, heat-treatment, and grinding station so non-conforming components never advance downstream.
Do Not Accept Non-Conforming Steel
Every incoming steel bar, forging, and cage blank undergoes chemical composition and metallographic screening before entering the machining line.
Do Not Manufacture Defects
First-piece inspection, patrol checks, and statistical process control (SPC) stabilize grinding wheel dress cycles, taper accuracy, and raceway crowning.
Do Not Release Unverified Lots
Finished assemblies are locked in quarantine until radial/axial clearance, vibration/noise checks, and final dimensional records are signed off.
Full Traceability & Root-Cause 8D
Zero concealment policy: any deviation triggers immediate segregation, 8D corrective analysis, and permanent preventive updates in FMEA control plans.
6-Stage Full-Process Quality Control Workflow
Every heavy-duty spherical, cylindrical, tapered, four-row rolling mill, and precision ball bearing passes six documented control checkpoints prior to export shipment.
Raw Bearing Steel & Chemistry
Material integrity determines rolling contact fatigue life. We verify melt composition and cleanliness before rough turning begins.
- Direct-reading spectrometer alloy & trace-element checks
- Non-metallic inclusion & carbide banding inspection
- Lot heat-number stamping for full downstream traceability
Metallurgy & Hardness Control
Through-hardening and case-carburizing cycles for large rolling mill and crusher rings are audited for uniform microstructure and dimensional stability.
- Optical metallographic checks of martensite & retained austenite
- Rockwell & Vickers hardness profiling across ring cross-sections
- Decarburization depth and temper stability validation
Precision Grinding & Raceway Profile
Internal, external, and superfinishing operations are governed by first-piece verification and in-process patrol gauges.
- Bore, outside diameter, and width tolerance per ISO 492
- 1:12 (K) and 1:30 (K30) tapered bore angle gauge verification
- Logarithmic roller & raceway crowning to prevent edge stress
CMM Metrology & Clearance Matching
Temperature-stabilized metrology ensures accurate geometric runout and matched internal clearance groups before final assembly.
- CMM verification of cage pocket spacing, oil holes & Fw/Ew
- Roundness, cylindricity, and Ra surface roughness scans
- CN, C3, C4, and custom drawing radial/axial clearance setup
Non-Destructive Testing (UT & MPI)
Heavy-section forgings and ground raceways undergo non-destructive screening per batch control plan or customer engineering drawing.
- Ultrasonic testing (UT) for subsurface inclusions & voids
- Magnetic particle inspection (MPI) for grinding burns & microcracks
- Strict demagnetization control after magnetic inspection
Cleaning, Preservation & Export Crating
Finished bearings are ultrasonically washed, preserved against maritime humidity, and packed with full inspection documentation.
- Residual magnetism check and smooth manual rotation audit
- Anti-rust oil coating, VCI barrier wrap & sealed export cases
- Factory dimensional & clearance inspection report matched by lot
Real Factory Inspection & Testing Equipment
All photographs below are authentic factory shots from our group manufacturing and metrology facilities, covering chemical composition, metallography, coordinate geometry, surface texture, and non-destructive testing.
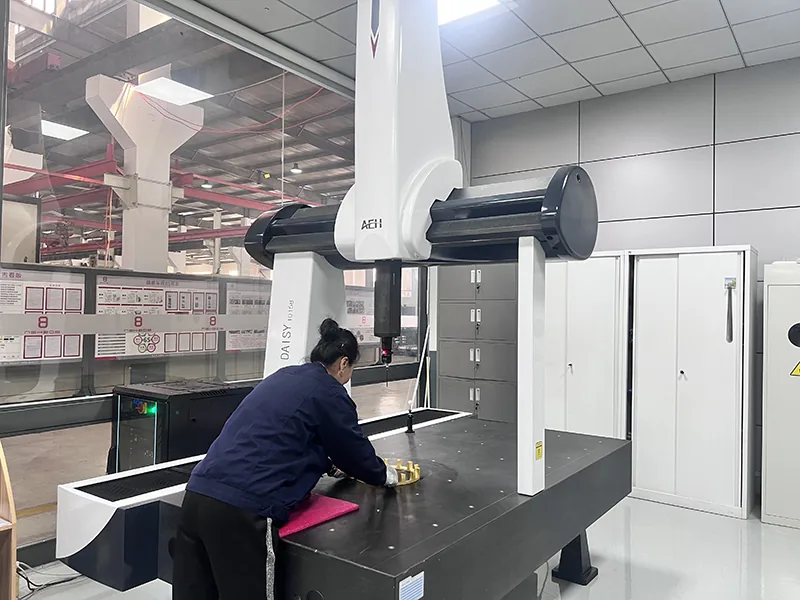
Bridge Coordinate Measuring Machine (CMM)
Contact-probe 3D verification of complex bearing rings, four-row mill spacers, machined brass cages, concentricity, and geometric runout.
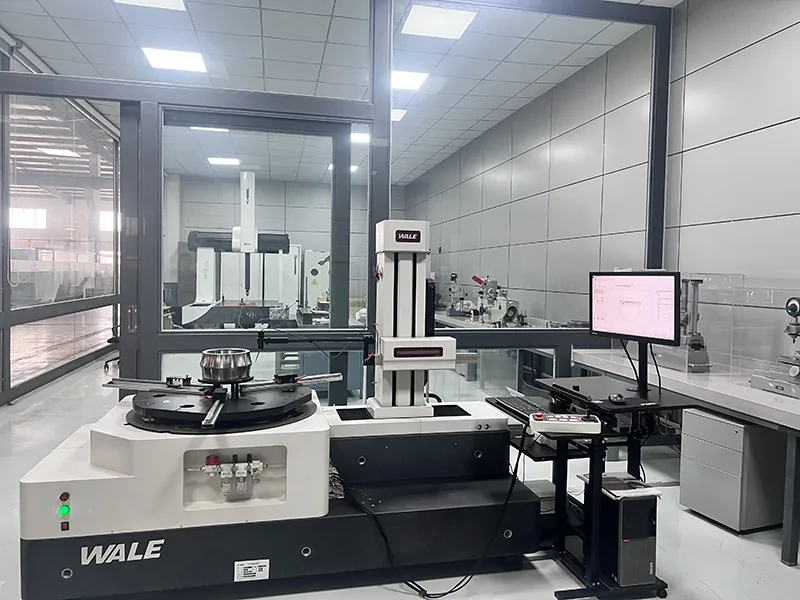
Precision Roundness & Cylindricity Analyzer
High-accuracy rotary-table evaluation of raceway roundness, lobing, coaxiality, and radial runout across large industrial bearing rings.
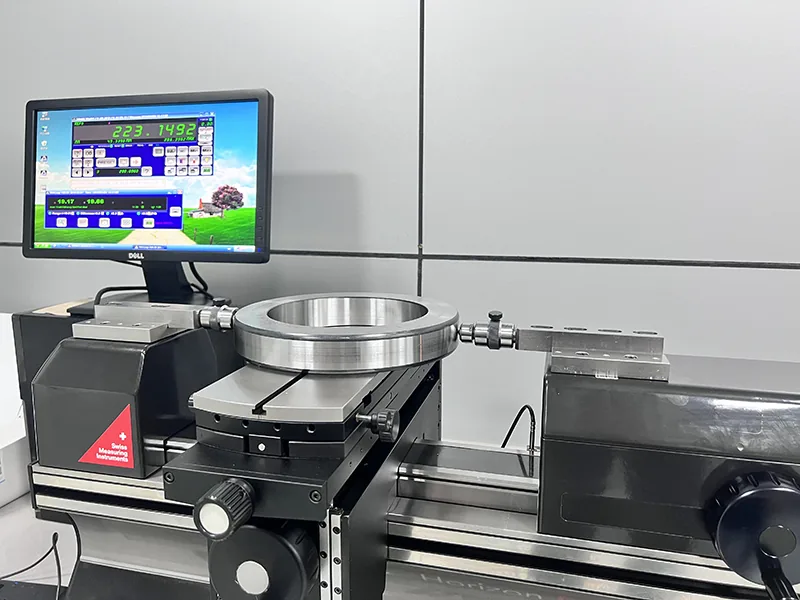
Swiss Horizontal Length Measuring Machine
Sub-micron verification of bore/OD dimensions, roller diameter sorting grades, master setting rings, and production inspection gauges.
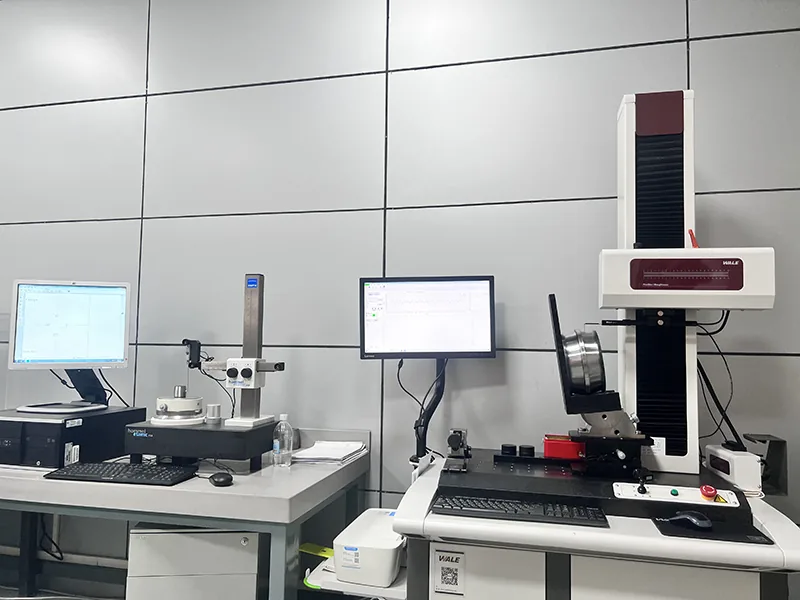
Contour & Surface Roughness Profilers
Measures raceway micro-roughness (Ra/Rz), roller logarithmic crowning profiles, rib angles, and chamfer geometry to optimize oil-film formation.
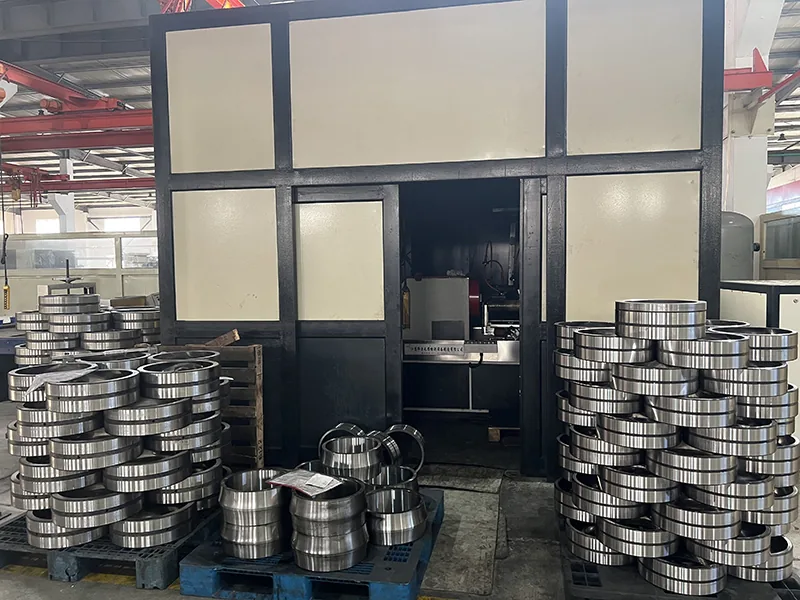
Ultrasonic & Magnetic Particle NDT Station
Dedicated darkroom magnetic particle (MPI) and ultrasonic (UT) screening to detect subsurface steel inclusions and surface microcracks on heavy rings.
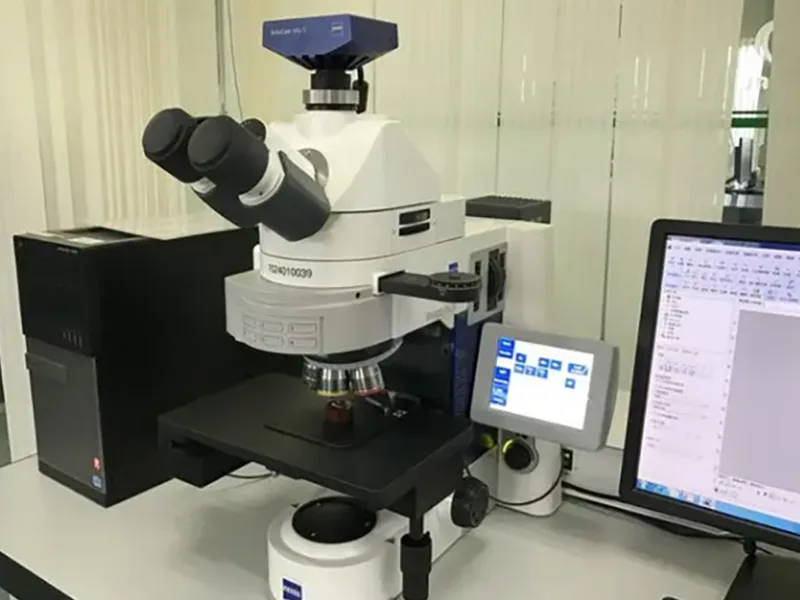
Zeiss Optical Metallographic Microscope
Evaluates raw steel inclusion cleanliness, carbide network/banding, annealing spheroidization, and quenched martensitic microstructure.
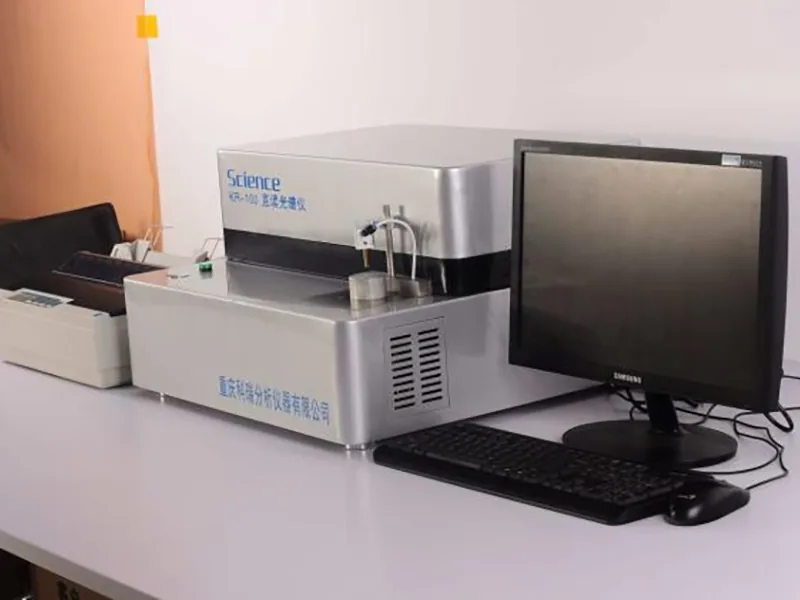
Direct Reading Optical Spectrometer
Quantifies carbon, chromium, manganese, silicon, and trace impurity elements in incoming bearing steel heats before release to forging and turning.
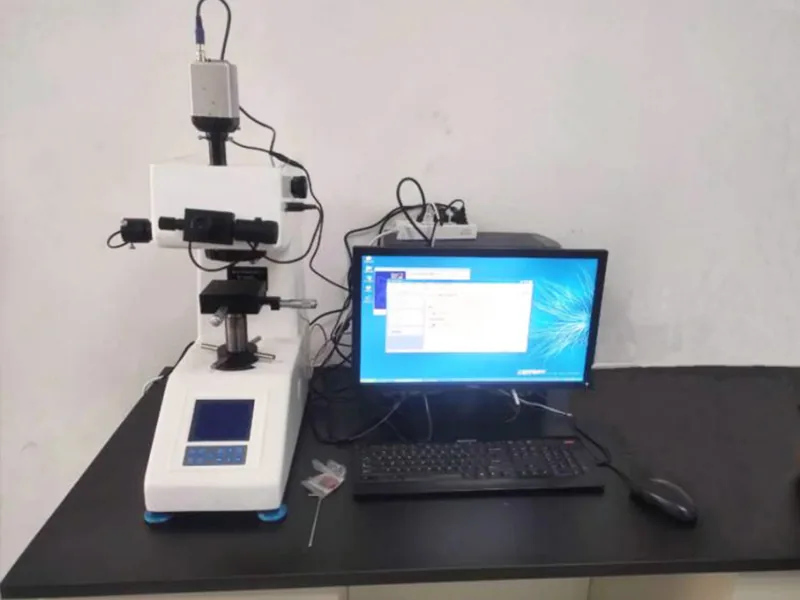
Digital Rockwell & Vickers Hardness Testers
Confirms ring and roller surface hardness uniformity, effective case-hardening depth on carburized mill bearings, and temper consistency.
Inspection Standards & Shipment Documentation Matrix
Transparent inspection scope tailored for global OEM purchasing teams and heavy-industry MRO engineers. Additional drawing-specific tests or third-party witness inspections are confirmed at quotation stage.
| Inspection Category | Primary Parameters Verified | Reference Standards | Available Buyer Documentation |
|---|---|---|---|
| Boundary & Running Accuracy | Bore (d), OD (D), width (B/T/H), taper angle (1:12 K / 1:30 K30), radial & axial runout | ISO 492 / ISO 199 (P0, P6, P5 per drawing) | Factory Dimensional Inspection Sheet (lot-traceable) |
| Internal Clearance & Assembly | Unmounted radial internal clearance (CN, C3, C4), four-row Fw/Ew matching, axial play | ISO 5753-1 & ZQM Engineering Drawing | Pre-shipment Clearance & Matching Record |
| Material & Metallurgy | Steel alloy chemistry, carbide & inclusion rating, quenched microstructure, Rockwell/Vickers hardness | ISO 683-17 / Factory Metallurgy Spec | Batch Hardness & Factory Material Verification Record |
| Non-Destructive Testing (NDT) | Subsurface ultrasonic flaw detection (UT) & magnetic particle surface crack inspection (MPI) | Per Heavy-Duty Lot Plan or Customer Drawing | NDT Inspection Summary (confirmed upon order) |
| Third-Party Witness Inspection | Pre-shipment dimensional audit, packaging verification, and test witnessing | Buyer Protocol (SGS / BV / TUV / Client QC) | On-site Factory Audit & Witness Support in Wafangdian |
Frequently Asked Questions on ZQM Quality Control
What quality management certifications does ZQM Bearings hold?
ZQM Bearings operates under certified ISO 9001 quality management and ISO 14001 environmental management systems across our Wafangdian manufacturing operations, supported by APQP, FMEA, SPC, and 8D corrective control workflows.
Which inspection records are supplied with export bearing orders?
Standard export shipments include a lot-traceable factory dimensional and internal clearance inspection report. Additional metallurgical, hardness, roundness, CMM, or ultrasonic/magnetic NDT reports can be scoped and confirmed per your purchase drawing prior to production.
How do you verify clearance and Fw matching on four-row rolling mill bearings?
Four-row cylindrical (FC/FCD/FCDP) and four-row tapered (TQO) bearings are matched as complete numbered sets. We inspect bore, OD, total width, roller envelope diameter (Fw), and matched radial or axial internal clearance on calibrated gauges and CMM stations before final packing.
Can ZQM manufacture to tighter tolerance grades such as P6 or P5?
Yes. Standard industrial bearings are manufactured to ISO 492 Normal (P0) tolerance, while P6, P5, or custom non-standard dimensional tolerances (such as -0.5 mm special OD QJF housings or machine-tool NN30 spindles) are manufactured and inspected strictly against confirmed engineering drawings.
Do you support third-party pre-shipment inspection or factory audits?
Yes. International OEMs and EPC buyers are welcome to schedule on-site factory audits at our Wafangdian manufacturing base or appoint independent third-party inspectors (such as SGS, BV, or TUV) to witness pre-shipment dimensional, hardness, and packaging checks.
Need Drawing-Specific Inspection or Third-Party Witnessing?
Share your bearing designations, tolerance class (P0 / P6 / P5), internal clearance (CN / C3 / C4), and required QC documentation. Our Wafangdian engineering and export desk responds within 24 hours.
- ISO 9001 & ISO 14001 Certified
- Factory Dimensional & Clearance Sheets
- Drawing-Based NDT & Custom Tolerance
- OEM & MRO Direct Supply