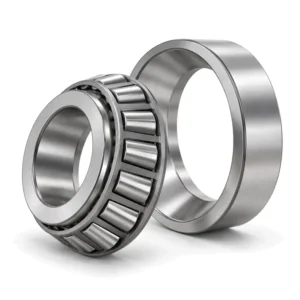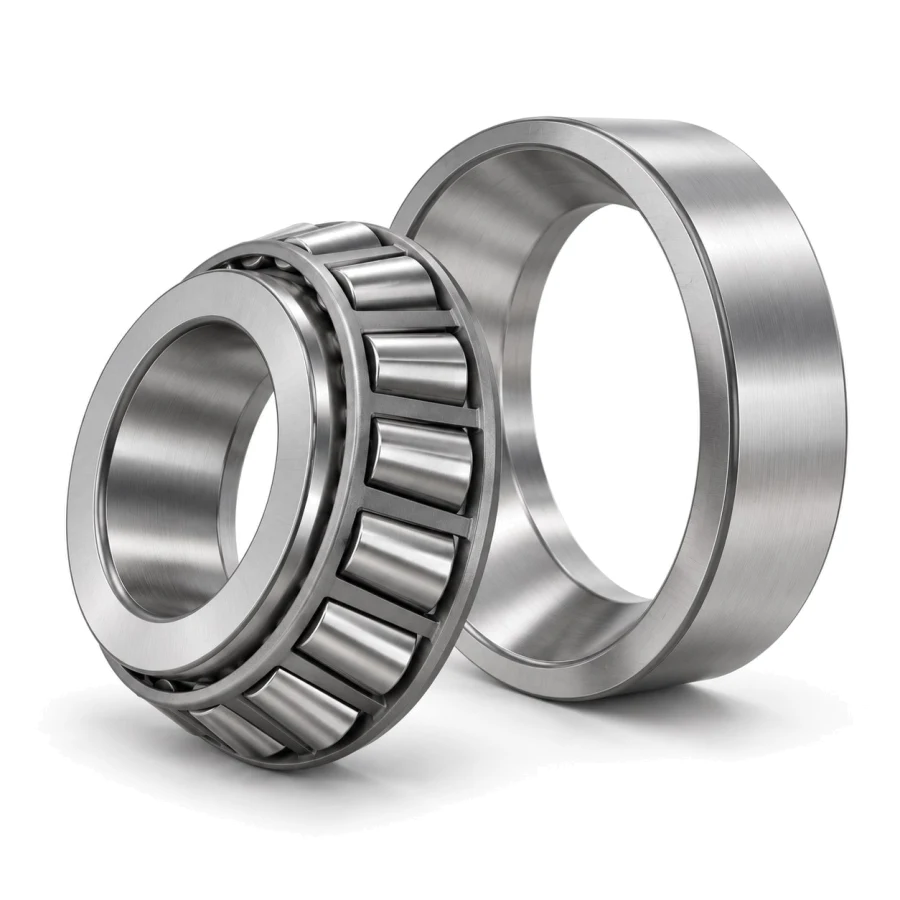
Packing a stiff 130 mm hollow central quill—complete with hydraulic fixture rotary unions, optical encoder cables, and drawbar actuation—inside a CNC horizontal boring mill rotary indexing table leaves precious little radial room for heavy castings. Engineered to the ISO 355 extra-light 329 series, the ZQM 32926 tapered roller bearing condenses 198 kN dynamic capacity (Cr) and 365 kN static rigidity (C0r) into a slender 130 × 180 × 32 mm footprint (25 mm radial wall height, cone width B = 32 mm, cup width C = 25 mm) weighing just 2.40 kg.
32926 Technical Specifications & Dimensions
| Parameter Category | Technical Parameter (Symbol) | Catalogue Reference Value |
|---|---|---|
| Boundary Dimensions & Weight | Bore diameter (d) | 130 mm |
| Boundary Dimensions & Weight | Outside diameter (D) | 180 mm |
| Boundary Dimensions & Weight | Inner-ring width (B) | 32 mm |
| Boundary Dimensions & Weight | Overall width (T) | 32 mm |
| Boundary Dimensions & Weight | Outer-ring width (C) | 25 mm |
| Boundary Dimensions & Weight | Reference mass (Weight) | 2.4 kg |
| Load Ratings & Limiting Speeds | Basic dynamic load rating (Cr) | 198 kN |
| Load Ratings & Limiting Speeds | Basic static load rating (Cor) | 365 kN |
| Abutment & Fillet Dimensions | Shaft abutment diameter (da) | 139 mm |
| Abutment & Fillet Dimensions | Shaft abutment reference diameter (db) | 141 mm |
| Abutment & Fillet Dimensions | Housing abutment diameter (Da) | 167 mm |
| Abutment & Fillet Dimensions | Housing abutment reference diameter (Db) | 173 mm |
| Abutment & Fillet Dimensions | Minimum chamfer dimension (r12) | 2 mm |
| Abutment & Fillet Dimensions | Minimum flange chamfer (r34) | 1.5 mm |
| Abutment & Fillet Dimensions | Maximum fillet radius (ra) | 1.5 mm |
| Abutment & Fillet Dimensions | Maximum flange fillet radius (rb) | 1.5 mm |
| Abutment & Fillet Dimensions | Load center distance (a) | 31 mm |
| Calculation Factors | Calculation factor (e) | 0.33 |
| Calculation Factors | Axial load factor (static) (Y0) | 1 |
| Calculation Factors | Axial load factor (Y) | 1.8 |
Data source: ZQM Bearings online catalogue database (factory PDF catalogue v1). Load ratings, limiting speeds, and parameters without individual test records serve as catalogue reference values; verify shaft/housing shoulders (da, db, Da), tolerances, internal clearance, and drawings prior to ordering.
Thin-Wall Stiffness & Preload Dynamics of 32926 in Precision Tables
Compared to conventional medium-section 130 mm tapered bearings, the 32926 trades 50 mm of outer-diameter bulk for agile low-inertia indexing while preserving true line-contact cutting rigidity:
- 25 mm Radial Cross-Section Economy: Housing pockets stay compact around the 180 mm outer diameter so worm-wheel gear rings and hydraulic clamping cylinders fit closer to the table rotation axis, slashing cantilevered overhang.
- High Axial Rigidity Ratio (e = 0.33, Y = 1.8): A shallower contact angle yields strong radial positioning fidelity during side-milling cuts while maintaining Y = 1.8 axial calculation precision under vertical plunge boring forces.
- Compact Load Apex Offset (a = 31.0 mm): Placing a matched pair of 32926 bearings with precision-ground inner and outer spacer rings creates a rigid zero-backlash spindle cartridge across minimal axial stack height.
- 365 kN Clamping & Indexing Stability: Heavy multi-ton workpieces indexed at low rpm demand high static indentation resistance so table positioning repeatability stays micron-true over years of pallet swaps.
ISO 355 Dimensional Equivalence Table for 32926
| Maker | Model Number | Bore d | OD D | T / B / C | Machine-Tool Notes |
|---|---|---|---|---|---|
| ZQM | 32926 | 130 mm | 180 mm | 32 / 32 / 25 mm | ISO 355 thin-wall base; P6/P5 precision confirmed per quote |
| SKF | 32926 | 130 mm | 180 mm | 32 / 32 / 25 mm | Extra-light metric single-row tapered roller |
| FAG / Schaeffler | 32926 | 130 mm | 180 mm | 32 / 32 / 25 mm | Precision rotary-table & hollow-spindle series |
| NSK | HR32926J | 130 mm | 180 mm | 32 / 32 / 25 mm | High-capacity thin-section metric execution |
| NTN / Koyo | 4T-32926 / 32926JR | 130 mm | 180 mm | 32 / 32 / 25 mm | Low-profile tapered assembly for indexers |
Precision substitution boundary: Nominal ISO 355 boundary alignment (130 × 180 × 32 mm) serves for envelope lookup only and does not guarantee equivalent runout class or torque uniformity. Rotary-table rebuilds must verify precision tolerance grade (such as P5 or P4) and matched-spacer preload calibration with the OEM drawing before swapping brands.
Precision Grinding Tolerances & Spacer-Ring Preload Procedure
- Decouple ISO 286-1 Dimensional Fits from ISO 1101 Geometry: Thin-section rings with a 25 mm radial wall telegraph every micron of mating seat imperfection directly onto the rollers. Grind the 130 mm cylindrical hollow-spindle journal and 180 mm table bore to ISO 286-1 IT5 dimensional limits, and separately certify ISO 1101 circularity, cylindricity, and shoulder axial runout to protect finish-machined workpiece roundness.
- Hold Exact Thin-Wall Abutments & Corner Fillets: Machine shaft shoulders to da = 139 mm and table housing shoulders to Da = 167 mm, keeping corner fillets safely inside the rmin = 2.0 mm minimum chamfer so the 32 mm cone and 25 mm cup sit dead square.
- Dial In Axial Preload via Ground Spacer Rings—Zero Feeler Gauges: Never check a thin-section tapered roller bearing with a radial feeler gauge. Assemble opposing 32926 units with lapped center spacer rings (or calibrated precision locknuts), spin the rotary table to settle roller skew, and tune final axial preload exclusively by measuring breakaway/running friction torque and axial elastic deflection under a test load.
- Guard Against Thermal Expansion Preload Spikes: In continuous turning-milling rotary tables, inner spindle heating faster than the cooled cast bed increases preload; validate thermal growth compensation during factory warm-up tests.
Low-Drag Lubrication & Coolant-Exclusion Strategy
Rotary indexing tables alternate between near-static heavy clamping and rapid 90°/180° indexing moves, exposing the 32926 to fretting corrosion and water-soluble metalworking coolant ingress. Apply metered low-viscosity synthetic barium-complex or lithium-complex precision spindle grease (25–30% cavity fill) for intermittent indexing, or recirculating ISO VG 32/46 filtered spindle oil for continuous mill-turn C-axis contouring. Pair top table joints with air-purged labyrinth seals to block fine cast-iron swarf and alkaline flood coolant.
Machine-Tool Rebuild Readiness & Quotation Intake
When quoting 32926 replacements for a boring-mill table or hollow-quill spindle rebuild, prepare four engineering parameters: (1) required precision grade (P0, P6, or P5 runout tolerance), (2) target preloaded torque or spacer-ring grinding gap, (3) continuous contouring rpm versus intermittent indexing duty, and (4) seal/lubrication scheme. Share your spindle drawing and batch quantity through our ZQM precision-bearing engineering desk.
Precision Selection & Reference: Decode precision and cage suffixes with the Bearing Suffix Decoder, inspect dimensional records on the 32926 Catalog Page, browse Tapered Roller Bearings, or review rotary-table bearing guides in Precision Machine Tools.
CNC Rotary Table & Hollow Spindle 32926 FAQ
Why does a CNC boring-mill rotary table choose 32926 over a standard 32226 on a 130 mm shaft?
Both share a 130 mm cylindrical bore, yet the 32926 trims outer diameter from 230 mm down to 180 mm and height from 67.75 mm to 32 mm, dropping mass from 11.0 kg to 2.40 kg. That 25 mm radial cross-section frees vital space for rotary hydraulic unions, direct-drive torque motors, and compact table bases.
How is preload calibrated on a paired 32926 hollow spindle without a feeler gauge?
Technicians lap matched inner and outer spacer rings (or adjust a precision locknut) while tracking spindle rolling torque and axial lift with a micron-resolution dial indicator. Radial feeler gauges cannot enter or measure tapered roller contact preload accurately.
Why are ISO 1101 form tolerances emphasized alongside ISO 286-1 IT5 fits for the 32926?
ISO 286-1 IT5 governs only the diameter size window, whereas ISO 1101 controls roundness, cylindricity, and face runout. A thin 25 mm ring conforms immediately to any three-lobed bore error, ruining rotary table indexing accuracy even when average bore diameter is within IT5.
What causes false brinelling on 32926 rollers inside an indexing table?
Heavy milling chatter transmitted into a stationary clamped table vibrates loaded rollers across a fixed microscopic arc, squeezing grease out of line contacts. Specifying anti-wear EP precision grease and performing periodic full-360° lubricating rotations prevents false brinelling grooves.