

Steel, Metallurgy and Rolling Mill Bearings
Engineered for integrated steelworks, hot and cold strip mills, aluminum rolling plants, and continuous slab casters. ZQM supplies straight-bore FC / FCD / FCDP four-row cylindrical, TQO / TQI four-row tapered, and large-bore 230 / 240 / 241 spherical roller bearings with verified catalogue tolerances and chock-ready consistency.
Bearing Selection by Steel Mill & Caster Position
Match roll-neck chocks, continuous caster segments, pinion stands, and heavy mill drives to verified ZQM roller bearing architectures.

Four-row straight-bore FC / FCD / FCDP cylindrical roller bearings carry extreme radial separating loads inside compact chock sections while allowing rapid roll-change swaps. Pair with dedicated thrust bearings in the chock for bidirectional axial control.
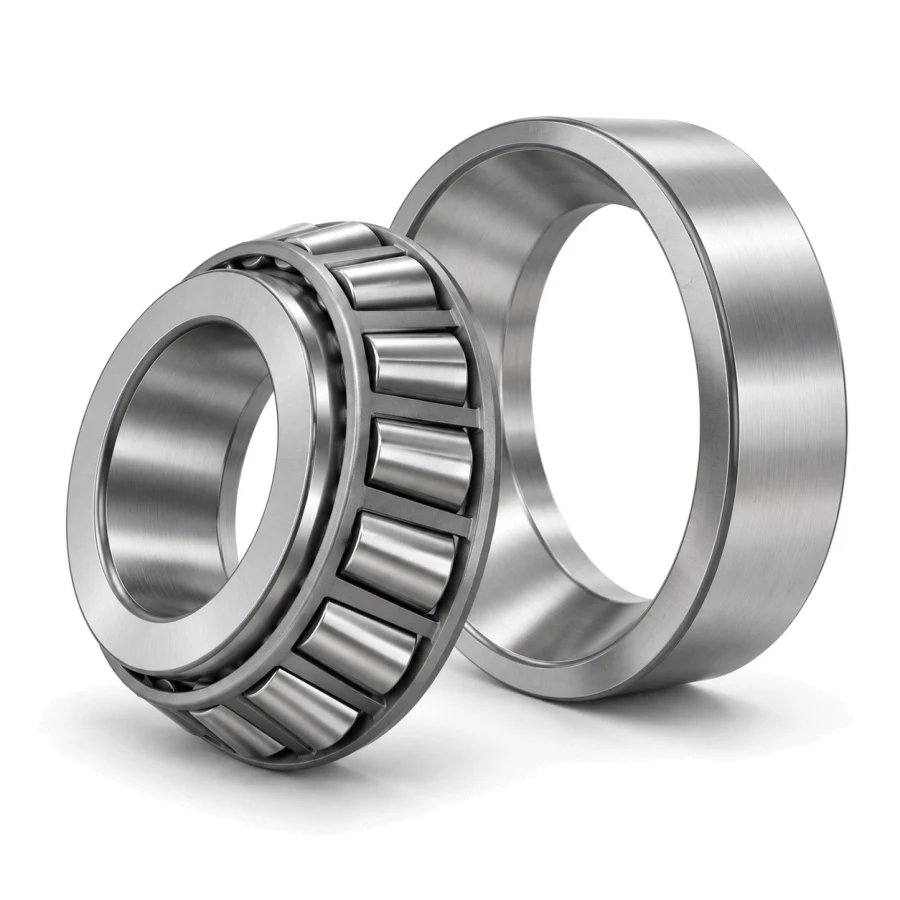
Where a single bearing assembly must locate the roll axially in both directions under combined separating and axial loads, TQO / TQI four-row tapered roller units and heavy 322 / 323 tapered roller sets handle roll-neck and auxiliary thrust duties per ISO 355.
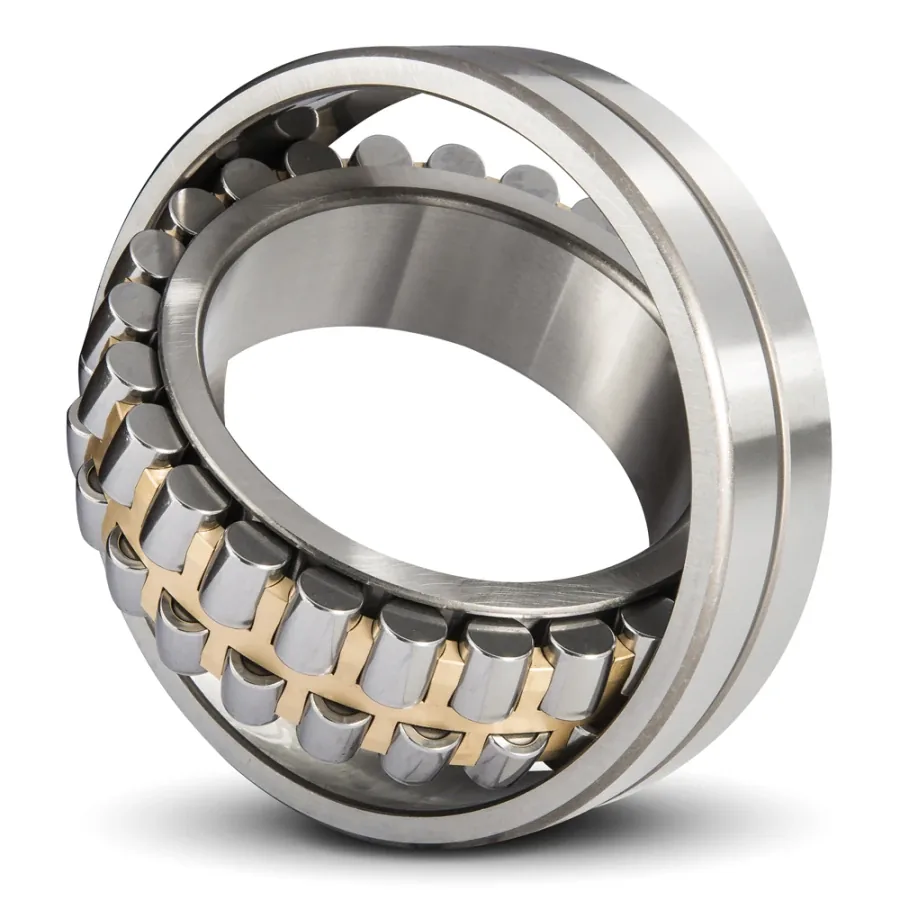
Low-speed, high-heat caster segment rolls, coiler mandrels, and converter trunnions face radiant slab heat, cooling spray, and structural deflection. Large-bore 230 / 231 (optional 1:12 K) and wide 240 / 241 (optional 1:30 K30) spherical bearings provide self-aligning durability.
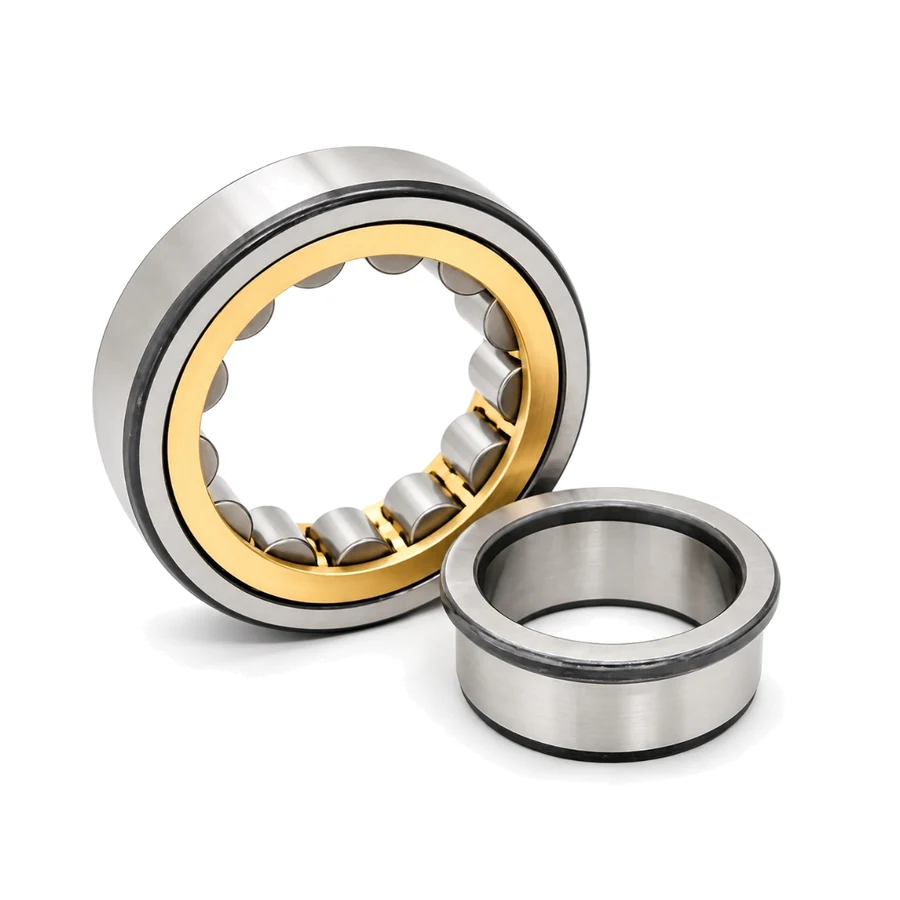
High-torque mill pinion stands and hot runout roller tables require separable straight-bore NJ / NU cylindrical roller bearings (NJ locating axially in one direction; NU floating thermal expansion within permissible limits) paired with heavy 231 / 232 spherical output bearings.
| Model | Series / Design | Dimensions (d × D × B/T) | Basic Load Cr / C0r | Ref. Mass | Typical Steelworks Position | Datasheet |
|---|---|---|---|---|---|---|
| FCD5678275 | Four-Row Cylindrical (Fw=308) | 280 × 390 × 275 mm | 2,720 / 6,130 kN | 105 kg | Hot/cold strip work & backup roll necks | View Spec |
| FCD4468210 | Four-Row Cylindrical (Fw=250) | 220 × 340 × 210 mm | 1,910 / 3,850 kN | 70.5 kg | Section & medium-plate roll necks | Catalog |
| FCDP4468290 | Pin-Cage Four-Row (Fw=250) | 220 × 340 × 290 mm | 2,980 / 5,010 kN | 96.5 kg | High-load wide-face rolling stands | Catalog |
| 220TQO320-3 | Four-Row Tapered (TQO) | 220 × 320 × 250 mm (T) | Per drawing / catalog | 68.0 kg | Combined radial + axial roll-neck chocks | Catalog |
| 23080 CA/W33 | Large Spherical (230, 1:12 K opt.) | 400 × 600 × 148 mm | 2,970 / 5,900 kN | 146 kg | Continuous caster rolls & ladle turrets | View Spec |
| 23084 CA/W33 | Large Spherical (230, 1:12 K opt.) | 420 × 620 × 150 mm | 2,910 / 5,850 kN | 151 kg | Heavy converter trunnions & drives | View Spec |
| 24152 CA/W33 | Wide Spherical (241, 1:30 K30 opt.) | 260 × 440 × 180 mm | 2,560 / 4,700 kN | 109 kg | Slab caster segments & heavy coilers | View Spec |
| 24060 CA/W33 | Wide Spherical (240, 1:30 K30 opt.) | 300 × 460 × 160 mm | 2,310 / 4,600 kN | 93.6 kg | Caster guide rolls & tension reels | View Spec |
| 23160 CA/W33 | Heavy Spherical (231, 1:12 K opt.) | 300 × 500 × 160 mm | 2,670 / 4,800 kN | 125 kg | Mill main reducer output shafts | View Spec |
| NJ326EM | Single-Row Cylindrical (Straight Bore) | 130 × 280 × 58 mm | 615 / 735 kN | 19.5 kg | Pinion stands & hot runout roller tables | View Spec |
| 32324 | Heavy Tapered (323, B=86 / C=69) | 120 × 260 × 90.5 mm (T) | 770 / 1,060 kN | 21.8 kg | Pinion bevel shafts & auxiliary thrust | View Spec |
Engineering Notice: Nominal boundary dimensions follow ISO 15 (radial) and ISO 355 (tapered overall width T). Cross-references to international mill designations match nominal envelope dimensions only; always verify under-roller diameter Fw, cage execution, lubrication grooves, and radial clearance or axial setting per mill chock drawing before installation.
Four Critical Engineering Checks for Steel Mill Bearings
Prevent premature roll-neck spalling, chock seizure, and unplanned mill shutdowns by confirming these parameters during specification.
1. Separable Fw & Radial Clearance Control (C3 / C4)
Hot-strip and continuous-caster shafts experience substantial thermal gradients between the hot roll neck and water-cooled chock housing. Specify C3 or C4 unmounted radial clearance based on interference-fit expansion and shaft-to-housing temperature delta, and confirm exact Fw whenever separable four-row inner rings remain on spare rolls.
Read Rolling Mill FCD / FCDP Guide2. Tapered Bore Discipline: 1:30 (K30) vs 1:12 (K) vs Straight Bore
Do not mix sleeve taper ratios across mill equipment. Wide 240 and 241 series spherical bearings use a 1:30 taper (K30) when ordered with tapered bores, while 230, 231, and 232 series use a 1:12 taper (K). Standard FC/FCD/FCDP four-row roll-neck bearings and NJ/NU pinion bearings use straight cylindrical bores unless a dedicated tapered roll-neck drawing is specified.
Read K vs K30 Tapered Bore Guide3. Axial Setting on Tapered Roll Necks & Thrust Pairing
Four-row FC/FCD/FCDP cylindrical bearings carry radial load only and require a separate thrust bearing in the chock. On TQO/TQI four-row tapered units and opposed 322/323 bevel-shaft pairs, set internal axial clearance or preload via matched spacer rings and axial end-play checks—never via radial feeler gauges.
Read Tapered Preload & Axial Setting Guide4. Scale, Cooling Water & Oil-Air Lubrication Protection
Mill scale and high-pressure descaling water accelerate abrasive wear and moisture corrosion. Combine W33 lubrication grooves and outer-ring oil holes with chock oil-air, oil-mist, or continuous EP grease purging and multi-lip chock seals to maintain stable lubricant film thickness under shock loads.
Read Heavy Bearing Damage Analysis
Rolling Mill & Caster RFQ Checklist
Include these 5 items in your inquiry so our bearing engineers can verify interchangeability and lead time without back-and-forth delays:
- Complete Designation or Drawing: Original bearing code or roll-neck drawing with d × D × B/T and separable Fw.
- Stand & Operating Position: Hot/cold work roll, backup roll, continuous caster segment, converter trunnion, or pinion stand.
- Bore, Clearance & Cage Execution: Straight bore vs K (1:12) / K30 (1:30), C3 / C4 clearance, solid brass or pin-type cage.
- Lubrication & Thermal Conditions: Oil-air, oil-mist, circulating oil, or EP grease, plus expected roll-neck operating temperature.
- Order Volume & Delivery Target: Trial chock set or scheduled plant maintenance batch, destination port, and inspection scope.
Steel & Rolling Mill Bearing FAQs
Practical engineering answers for steelworks maintenance engineers and OEM rolling-mill procurement teams.
When should rolling mill stands use FC / FCD / FCDP four-row cylindrical bearings instead of TQO four-row tapered bearings?
Use FC, FCD, or FCDP four-row cylindrical roller bearings when work or backup roll necks require maximum radial capacity inside a compact section and high roll-change speed (separable straight-bore inner rings stay on the roll neck). Because four-row cylindrical bearings take radial load only, they must pair with a separate axial thrust bearing (such as double-direction tapered roller thrust, four-point contact ball, or deep-groove ball locating bearings) in the chock. Choose TQO / TQI four-row tapered roller bearings when a single compact roll-neck assembly must support both high radial separating force and bidirectional axial thrust.
Why is roller under-diameter (Fw) verification mandatory when replacing separable four-row rolling mill bearings?
In hot and cold rolling mills, roll-neck inner rings remain interference-fitted on spare roll shafts while outer-ring/roller assemblies rotate between chocks. Interchanging assemblies across mill stands or brands requires verifying the exact under-roller raceway diameter Fw (for example, Fw = 308 mm on FCD5678275 or Fw = 250 mm on FCD4468210) and matched radial internal clearance—matching nominal d × D × B alone is not sufficient for separable chock interchangeability.
How do tapered bore ratios differ between 240/241 continuous caster bearings and 230/231/232 mill drive bearings?
Standard catalog units in these spherical series are supplied with straight cylindrical bores. Where sleeve-mounted tapered bores are specified, wide-section 240 and 241 series bearings use a 1:30 taper (K30), whereas 230, 231, and 232 series bearings use a 1:12 taper (K). Four-row FC/FCD/FCDP cylindrical bearings and NJ/NU pinion bearings use straight cylindrical bores unless a dedicated tapered roll-neck drawing is engineered.
What engineering details should steelworks OEMs and MRO buyers send for a rolling mill bearing quotation?
Provide the full original bearing designation or roll-neck drawing (including bore, OD, total width B or T, Fw, radial clearance group C3/C4, cage design, and lubrication holes/grooves), mill stand position (work roll, backup roll, continuous caster, or pinion stand), lubrication method (oil-air, oil-mist, circulating oil, or EP grease), and batch quantity. ZQM verifies boundary tolerances, clearance, and inspection scope before quoting.
Related Metallurgy & Rolling Mill Engineering Guides
Technical references from the ZQM engineering library covering roll-neck architecture, sleeve tapers, and ISO cross-referencing.
Need Technical Verification for Rolling Mill or Caster Bearings?
Share your bearing designations, roll-neck drawings, Fw / clearance specifications, and maintenance schedule. ZQM’s engineering and export team will confirm exact dimensional matching and factory lead times.