

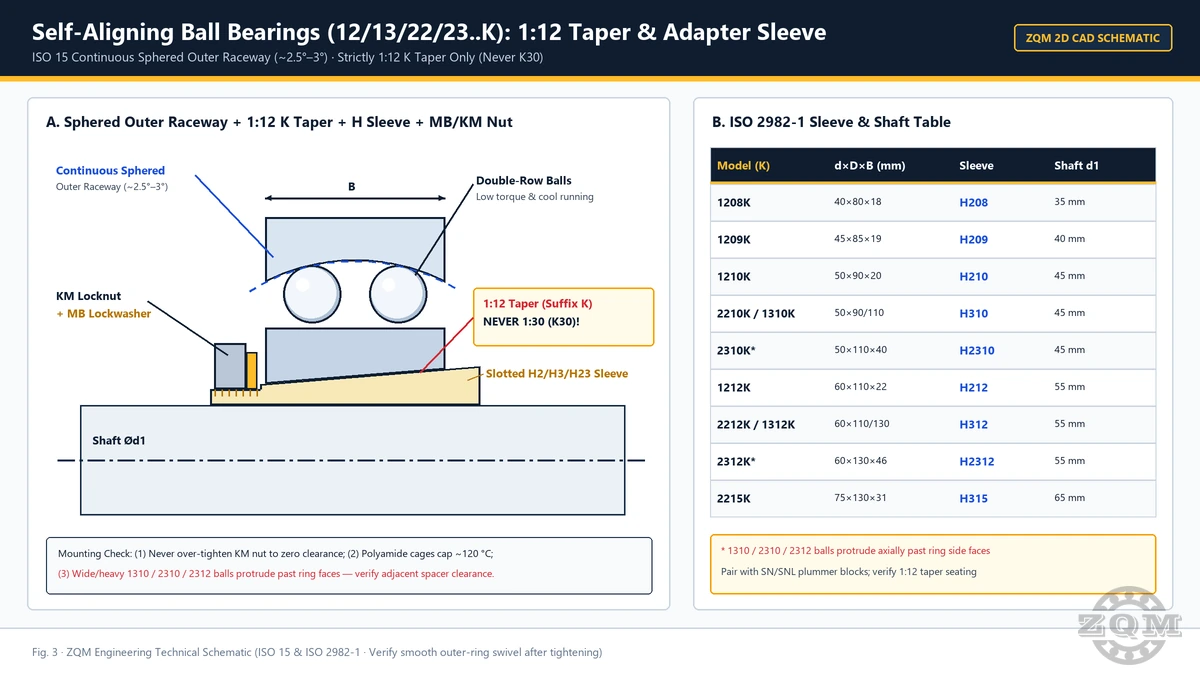
Across commercial HVAC air-handling fans, agricultural drive shafts, light-to-medium belt conveyors, and split SN / SNL plummer block housings, long shaft spans and fabricated steel frames inevitably introduce housing misalignment and shaft bending. ISO 15 double-row self-aligning ball bearings (12, 13, 22, and 23 series) solve that geometry challenge by pairing two rows of precision balls with a continuous sphered outer-ring raceway—accommodating roughly 2.5° to 3° of angular misalignment while generating remarkably low friction heat at elevated speeds. Yet most premature field failures do not come from fatigue; they come from mixing up cylindrical versus 1:12 tapered bores (K), mis-matching H2 / H3 / H23 adapter sleeves, over-tightening KM locknuts, or overlooking ball side protrusion on wide 13 and 23 units.
Why Self-Aligning Ball Bearings Excel on Long Shafts and Split Plummer Blocks
Unlike rigid deep groove ball bearings—which suffer rapid edge stress when a welded fan frame twists by even a fraction of a degree—an ISO 15 self-aligning ball bearing pivots freely around the bearing center inside its concave spherical outer raceway. Because point-contact ball kinematics generate lower rolling resistance than line-contact rollers, these bearings run noticeably cooler than spherical roller bearings on high-speed blowers, woodworking spindles, textile frames, and conveyor and bulk-handling shafts under light-to-moderate radial loads.
That structural freedom comes with two engineering boundaries you should respect during selection: first, axial load capacity is modest compared with angular contact or roller alternatives; second, radial internal clearance is relatively tight, making shaft fit and adapter sleeve drive-up precision decisive for service life.
1:12 Tapered Bore (K) vs Cylindrical Bore — and the Critical Taper Boundary
Every standard 12, 13, 22, and 23 series size is manufactured with either a straight cylindrical bore (no bore suffix) or a tapered bore designated by suffix K. Before machining a shaft or sourcing replacement sleeves, lock in one non-negotiable ISO standard rule:
Critical Taper Boundary: Tapered-bore self-aligning ball bearings (K) are strictly 1:12 taper ONLY—NEVER 1:30 (K30). The shallower 1:30 taper (K30) applies exclusively to wide 240 and 241 series spherical roller bearings. Attempting to seat a K self-aligning ball bearing onto a 1:30 shaft or sleeve causes immediate line-edge contact at one end of the bore and fractures the inner ring during tightening.
- Mounts directly onto a stepped, precision-ground shaft seat (typically
j5/k5/k6tolerance depending on load). - Requires shaft shoulders, circlips, or end plates for axial positioning; ideal for compact OEM fan hubs and gearboxes.
- Mounts anywhere along an unstepped commercial cold-drawn shaft (
h9/IT5–IT6) inside splitSN/SNLplummer blocks. - Eliminates shaft machining steps and lets maintenance crews lock axial position via the
KMlocknut andMBlockwasher.
Verified ISO 15 and ISO 2982-1 Dimension and Adapter Sleeve Reference Table
Selecting the wrong adapter sleeve series (for instance, pairing an H210 sleeve intended for narrow 1210K with a wider 2210K or 2310K bearing) leaves threads exposed or fails to support the full inner-ring width. The verified ISO 15 + ISO 2982-1 reference table below maps 12 core industrial models directly to their exact boundary dimensions (d × D × B), 1:12 tapered designations, matching H2 / H3 / H23 sleeves, and resulting plain shaft diameters (d1). Click any model to review full product details and order options:
| Cylindrical Model | ISO 15 Series | d × D × B (mm) | 1:12 Tapered Bore | ISO 2982-1 Sleeve | Shaft Ø d1 | Engineering Note |
|---|---|---|---|---|---|---|
| 1208 | 12 (ISO 02) | 40 × 80 × 18 | 1208K (1:12) |
H208 |
35 mm | Standard narrow profile |
| 1209 | 12 (ISO 02) | 45 × 85 × 19 | 1209K (1:12) |
H209 |
40 mm | Standard narrow profile |
| 1210 | 12 (ISO 02) | 50 × 90 × 20 | 1210K (1:12) |
H210 |
45 mm | Standard narrow profile |
| 1212 | 12 (ISO 02) | 60 × 110 × 22 | 1212K (1:12) |
H212 |
55 mm | Standard narrow profile |
| 1310 | 13 (ISO 03) | 50 × 110 × 27 | 1310K (1:12) |
H310 |
45 mm | Check ball side protrusion |
| 1312 | 13 (ISO 03) | 60 × 130 × 31 | 1312K (1:12) |
H312 |
55 mm | Heavy section; check side clearance |
| 2208 | 22 (ISO 22) | 40 × 80 × 23 | 2208K (1:12) |
H308 |
35 mm | Wide 02 OD; higher radial capacity |
| 2210 | 22 (ISO 22) | 50 × 90 × 23 | 2210K (1:12) |
H310 |
45 mm | Wide 02 OD; common SN/SNL fit |
| 2212 | 22 (ISO 22) | 60 × 110 × 28 | 2212K (1:12) |
H312 |
55 mm | Wide 02 OD; fan and conveyor duty |
| 2215 | 22 (ISO 22) | 75 × 130 × 31 | 2215K (1:12) |
H315 |
65 mm | Note 10 mm bore-to-shaft step |
| 2310 | 23 (ISO 23) | 50 × 110 × 40 | 2310K (1:12) |
H2310 |
45 mm | Wide heavy series; ball protrusion alert |
| 2312 | 23 (ISO 23) | 60 × 130 × 46 | 2312K (1:12) |
H2312 |
55 mm | Wide heavy series; ball protrusion alert |
Notice two practical patterns across the ISO 2982-1 sleeve series:
- Width-to-Sleeve Rule: Narrow
12series usesH2xxsleeves; both medium-heavy13series and wide22series shareH3xxsleeves; and wide-heavy23series requires longerH23xxsleeves to span the wider inner ring cleanly. - Bore-to-Shaft Step Change at Code 15: For bore codes
08through12(40–60 mm bearing bore), the adapter sleeve steps the plain shaft diameter down by5 mm(e.g.,60 mmbore fits a55 mmshaft). Starting at bore code15(2215K+H315), the sleeve wall thickens and steps down by10 mm(75 mmbore fits a65 mmshaft). Always confirm actual shaft diameterd1rather than assuming a constant 5 mm difference.
Step-by-Step H2 / H3 / H23 Adapter Sleeve, MB Lockwasher and KM Locknut Mounting Checklist
Because the 1:12 taper acts as a mechanical wedge, tightening the KM locknut expands the bearing inner ring outward and reduces radial internal clearance. Use our Tapered Bore Clearance Calculator to plan drive-up targets before assembly, and follow this five-step shop-floor sequence on every installation:
- Inspect and Lightly Oil the Shaft and Taper Interfaces: Confirm the plain shaft is free of burrs, scores, and taper errors. Wipe the outside of the
H2 / H3 / H23sleeve and the bearing1:12bore clean, then apply only a thin film of light machine oil to the taper—never thick grease, which causes unpredictable axial drive-up and risks sleeve slippage under load. - Position the Sleeve and Seat the Bearing Squarely: Slide the slotted adapter sleeve to its exact axial location on the shaft (remembering that the inner ring shifts slightly axially during tightening). Slide the
K-bore self-aligning ball bearing onto the taper, place theMBlockwasher with its inner tang engaged in the sleeve keyway, and thread theKMlocknut with its chamfered side facing the lockwasher and bearing. - Tighten Gradually Without Wiping Out Radial Clearance: Advance the
KMlocknut smoothly with a properly sized hook spanner—never hammer directly on nut slots with a chisel, which sends impact shocks straight into the ball raceways. Avoid over-tightening: unlike large spherical roller bearings where feeler gauges slide easily between rollers and outer ring, self-aligning ball bearings have tight radial clearances that vanish rapidly under excessive axial drive-up. - Verify Smooth Outer-Ring Swivel and Rotation by Hand: After seating the nut, rotate the outer ring and tilt it gently across its spherical raceway by hand. The outer ring must rotate smoothly and swivel effortlessly with zero binding or notchiness. If swiveling feels stiff or locked, radial internal clearance has been wiped out—back off the
KMlocknut immediately, release the inner ring slightly, and re-seat to restore free swivel. - Lock the MB Tab and Set Housing Axial Float: Once clearance and smooth swivel are verified, bend the aligned outer tab of the
MBlockwasher cleanly into the matchingKMlocknut slot. Never back off the nut just to align a slot; advance slightly if needed without causing bind. Finally, install stabilizing/locating rings in only one split plummer block (the locating bearing) while leaving the opposite bearing free to float axially in its housing seat to absorb shaft thermal growth.
Two Frequently Missed Engineering Checks: Ball Side Protrusion and Cage Thermal Limits
Even with a flawless sleeve fit, two physical design details on ISO 15 self-aligning ball bearings routinely catch maintenance teams off guard during retrofits:
- Ball Side-Protrusion Warning on Wide/Heavy Series (1310, 2310, 2312): On wider heavy-section models—including 1310, 2310, and 2312—the large-diameter double-row balls protrude axially slightly past the nominal width
Bof the inner and outer ring faces. When assembling these bearings next to custom stepped spacers, tight labyrinth seals, housing end covers, or oversized locknuts, measure axial side clearance explicitly so the rotating balls never contact adjacent stationary hardware. - Cage Material Thermal Awareness: Many modern self-aligning ball bearings are supplied with glass-fiber reinforced polyamide cages for quiet, low-inertia operation. Polyamide cages are typically capped around ~120 °C continuous operating temperature and may embrittle early in hot synthetic oils or high-EP-additive gear lubricants. For induced-draft hot-gas fans, kiln blowers, or elevated-ambient dryer shafts, request pressed steel or machined solid brass cages and confirm the exact cage execution against your order drawing rather than assuming cage material from a base model number.
Pre-Order Engineering Confirmation Checklist for B2B Buyers
To prevent dimension mismatches, sleeve returns, or thermal cage failures, include these six items when requesting a quotation from ZQM Bearings—each order follows our traceable factory inspection workflow outlined on our Quality and Inspection page:
- Full Designation and Bore Execution: Specify cylindrical bore (e.g.,
2212) or1:12tapered bore (2212K) explicitly. - Shaft Diameter and Sleeve Kit Scope: State plain shaft diameter
d1and whether you require the complete ISO 2982-1 kit (H2 / H3 / H23sleeve +MBlockwasher +KMlocknut). - Sealing and Lubrication Requirement: Confirm open execution (for relubricated plummer blocks) versus integral contact seals (
2RS) and grease temperature range. - Radial Internal Clearance Group: State
CN(standard) orC3(recommended for elevated fan duct heat or tighter shaft interference fits). - Cage Material and Operating Temperature: Flag continuous operating temperatures above
100–120 °Cor chemically aggressive lubricants so steel or brass cages can be confirmed upfront. - Adjacent Hardware Clearance: For
1310,1312,2310, and2312retrofits, note any close-clearance spacers or labyrinth seals next to the bearing faces.
Frequently Asked Questions
Do 12, 13, 22, or 23 series self-aligning ball bearings ever use a 1:30 (K30) tapered bore?
No. Every tapered-bore ISO 15 self-aligning ball bearing carries the suffix K and uses a 1:12 taper exclusively. The shallower 1:30 taper (suffix K30) is reserved for wide heavy-section 240 and 241 series spherical roller bearings and is never used on self-aligning ball bearings.
How do I match H2, H3, and H23 adapter sleeves to 12, 13, 22, and 23 series bearings?
Under ISO 2982-1, narrow 12 series K-bore bearings pair with H2xx sleeves (such as 1208K with H208 and 1212K with H212), medium-width 13 series and wide 22 series K-bore bearings pair with H3xx sleeves (such as 1310K or 2210K with H310, and 2215K with H315), and extra-wide heavy 23 series bearings pair with H23xx sleeves (such as 2310K with H2310 and 2312K with H2312).
Why should I verify smooth outer-ring swivel by hand after tightening the KM locknut on an adapter sleeve?
Self-aligning ball bearings start with smaller radial internal clearance than spherical roller bearings, and over-tightening the KM locknut drives the inner ring too far up the 1:12 taper, eliminating clearance and preloading the balls. Checking that the outer ring rotates smoothly and swivels freely by hand immediately confirms residual clearance remains intact before bending the MB lockwasher tab.
What is the ball side-protrusion hazard on wide 13 and 23 series self-aligning ball bearings?
On several larger or wider ISO 15 sizes—notably 1310, 2310, and 2312—the double-row balls protrude slightly beyond the nominal axial width B of the inner and outer ring side faces. Engineers must check adjacent shaft spacers, locating rings, locknuts, and labyrinth or V-ring seals to ensure adequate axial clearance so the balls never rub against neighboring components.
When should I specify a pressed steel or brass cage instead of a polyamide cage on a self-aligning ball bearing?
Standard glass-fiber reinforced polyamide cages run quietly with low friction but are generally limited to approximately 120 °C continuous operating temperature and can degrade in aged synthetic oils or aggressive EP additives at high heat. For hot-gas HVAC exhaust fans, drying tunnels, or higher-temperature industrial ducts, specify pressed steel or machined brass cages and confirm thermal ratings with engineering before ordering.
Sourcing ISO 15 Self-Aligning Ball Bearings or Matched H2 / H3 / H23 Sleeve Kits?
Share your bearing model (12 / 13 / 22 / 23 series), shaft diameter d1, cage temperature requirement, and plummer block housing code. ZQM engineers verify bore taper, sleeve compatibility, and order-matched inspection details before quoting.