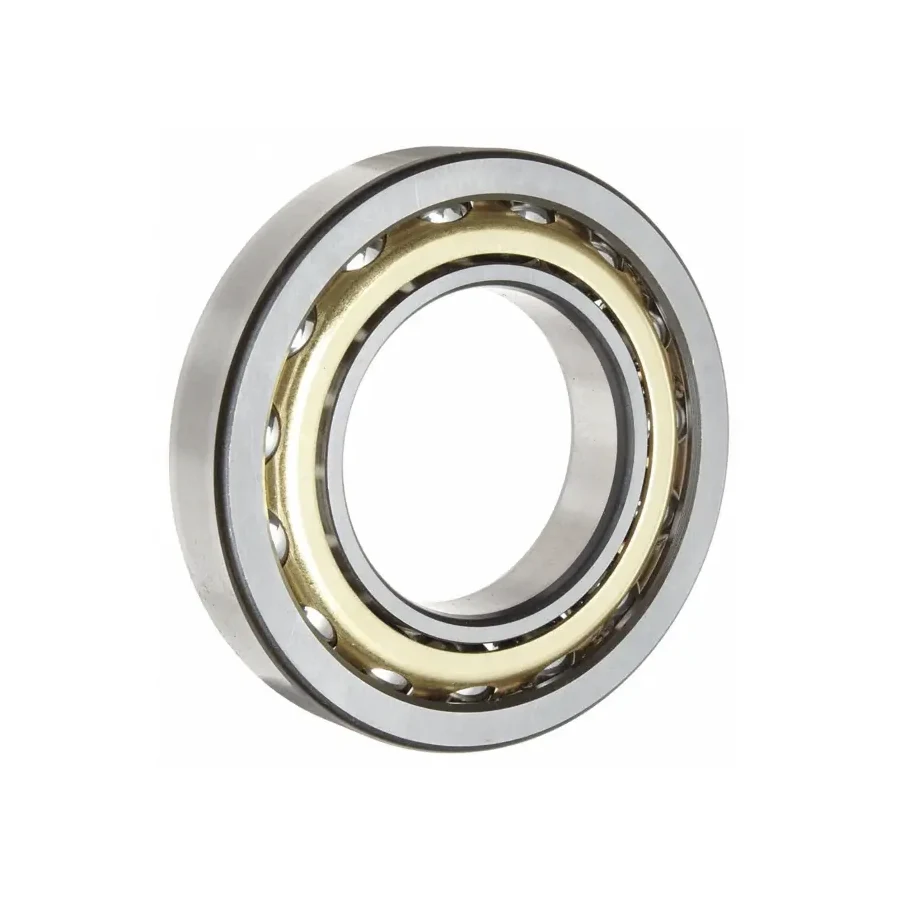
Tailored to ISO 10 light cross-section proportions at 140 × 210 × 33 mm and just 4.14 kg per ring, the 7028ACM (7028 ACM) single-row angular contact ball bearing yields a basic dynamic rating of 98 kN and a static rating of 137 kN. Combining a slim 35 mm radial wall height, a 25° contact angle (AC), and a precision machined brass cage (M), it excels in large-bore CNC turning center hollow bar-feed spindles, multi-passage hydraulic rotary unions, and pipe-threading headstock cartridges where maximum through-hole diameter must fit inside a tight cast housing.
7028ACM Technical Specifications & Dimensions
| Parameter Category | Technical Parameter (Symbol) | Catalogue Reference Value |
|---|---|---|
| Boundary Dimensions & Weight | Bore diameter (d) | 140 mm |
| Boundary Dimensions & Weight | Outside diameter (D) | 210 mm |
| Boundary Dimensions & Weight | Width (B) | 33 mm |
| Boundary Dimensions & Weight | Reference mass (Weight) | 4.14 kg |
| Load Ratings & Limiting Speeds | Basic dynamic load rating (Cr) | 98 kN |
| Load Ratings & Limiting Speeds | Basic static load rating (Cor) | 137 kN |
| Load Ratings & Limiting Speeds | Limiting speed (grease) | 2000 rpm |
| Load Ratings & Limiting Speeds | Limiting speed (oil) | 3000 rpm |
| Abutment & Fillet Dimensions | Shaft abutment diameter (da) | 150 mm |
| Abutment & Fillet Dimensions | Housing abutment diameter (Da) | 200 mm |
| Abutment & Fillet Dimensions | Minimum chamfer dimension (r12) | 2 mm |
| Abutment & Fillet Dimensions | Minimum flange chamfer (r34) | 1 mm |
| Abutment & Fillet Dimensions | Maximum fillet radius (ra) | 2 mm |
| Abutment & Fillet Dimensions | Load center distance (a) | 57.3 mm |
| Calculation Factors | Calculation factor (e) | 0.68 |
| Calculation Factors | Axial load factor (static) (Y0) | 0.38 |
| Calculation Factors | Axial load factor (Y) | 0.87 |
| Calculation Factors | Radial load factor (X) | 0.42 |
Data source: ZQM Bearings online catalogue database (factory PDF catalogue v1). Load ratings, limiting speeds, and parameters without individual test records serve as catalogue reference values; verify shaft/housing shoulders (da, db, Da), tolerances, internal clearance, and drawings prior to ordering.
7028ACM Compact 70-Series Wall Section & 25° Stiffness
Hollow-spindle oil-country lathes and large multi-port rotary unions need generous 140 mm internal shaft diameters to pass bar stock, draw-tubes, or pressurized coolant manifolds without bloating outer housing dimensions. At only 33 mm wide and 210 mm OD, the 7028ACM packs a high ball complement into a remarkably low-inertia cross-section.
- Cool-Running 25° Raceway (AC): Setting the contact angle at 25° places the effective load center at a = 57.3 mm with catalog calculation factors e = 0.68 and Y = 0.87. That geometry delivers crisp radial and axial cutting stiffness while limiting spin-friction heating at speeds up to 3,000 r/min (oil) or 2,000 r/min (grease).
- Multi-Bearing Spindle Stacks: A single 7028ACM resists axial cutting thrust in one direction only. Turning headstocks commonly deploy opposed back-to-back (DB) pairs or triplex DBD stacks (two tandem rings facing heavy chucking/facing cuts opposed by one preloading ring) to eliminate axial backlash.
- Machined Solid Brass Retainer (M): Resists centrifugal distortion and thermal softening across continuous unmanned bar-feeding shifts while running smoothly under fine oil-air mist.
Hollow Bar-Feed Spindle & Rotary Union Housing Precision
Thin-section 70-series rings copy the geometric roundness of the shaft and bore they sit against. If a hollow draw-tube spindle journal displays lobing or taper beyond precision grinding tolerances, pressing a 140 mm thin-walled inner ring onto it transmits uneven ball preload straight into the raceway, degrading machined surface finish and accelerating rotary-union mechanical-seal wear.
Grind mating spindle journals and housing cartridges to strict cylindricity while observing catalog abutment dimensions: minimum shaft shoulder da ≥ 150 mm, maximum housing shoulder Da ≤ 200 mm, and clean undercut relief clearing the r min = 2.0 mm ring chamfer. Measure locknut face runout prior to final spindle clamping so preload distributes evenly around all 360° of the 33 mm ring face.
Low-Churning Oil-Air Mist & Grease-Pack Thermal Control
Hollow turning spindles cycling rapidly between bar-index stops and 2,000–3,000 r/min finishing passes are highly sensitive to thermal spindle growth along the Z-axis. Over-filling a 7028ACM cavity with stiff general-purpose grease causes immediate churning heat; instead, technicians pack precisely metered low-viscosity synthetic spindle grease (typically 15–20% of free internal volume) followed by a staged step-speed run-in sequence.
For continuous multi-shift turning centers or high-RPM rotary coolant unions pushing near the 3,000 r/min oil ceiling, metered oil-air lubrication delivers micro-droplets right into the 25° contact zone while positive air pressure keeps water-soluble metalworking coolant out of the cartridge labyrinth.
7028ACM Brand Cross-Reference & Precision Verification
| Brand / Standard | Nominal Size Designation | Contact Angle & Series Remarks (140 × 210 × 33 mm) |
|---|---|---|
| ZQM / GB/T 292 | 7028ACM | 25° contact angle (AC), solid machined brass cage (M) |
| SKF | 7028 ACD / 7028 CD | ACD = 25° super-precision angle (verify cage material & tolerance class vs. industrial P0/P6/P5) |
| NSK | 7028A5 / 7028AM | A5 = 25° contact angle; verify brass vs. phenolic cage & precision grade |
| FAG / Schaeffler | B7028-E / 7028-B-MP | B7028-E uses 25° spindle geometry; 7028-B-MP is 40° industrial brass-cage series |
| NTN | 7028UAD / 7028L1 | Verify 25° vs. 30° contact angle, cage material, and flush-ground preload code |
Technical Equivalence Disclaimer: The table aligns strictly on ISO 15 Series 10 external boundaries (140 × 210 × 33 mm). Spindle and rotary-union builders must confirm accuracy class (P0/P6/P5/P4), contact angle (15° vs. 25° vs. 40°), cage material, and matched preload level directly against assembly blueprints before substitution.
Quoting 7028ACM Hollow-Spindle Sets with ZQM
Machine-tool OEMs, rotary-union engineers, and CNC spindle rebuilders quoting 7028ACM should share: target running accuracy class (P0, P6, or P5), matched set stack (DB, DF, DT, or triplex DBD), desired preload/clearance group, and lubrication system. ZQM provides batch-traceable dimensional, radial runout, and hardness inspection records for both single-spindle repair kits and scheduled OEM builds. Send your spindle drawing or inquiry through our engineering sales desk.
7028ACM Hollow Spindle & Rotary Union Q&A
Related Models & Engineering Tools: Need a heavier medium-section 25° unit? Compare 7224ACM (120 × 215 × 40 mm), explore spindle setups in Precision Machine Tools, verify operating life in our Bearing Life Calculator, decode precision tags via the Suffix Decoder, or browse all Angular Contact Ball Bearings.
Why choose the 70-series 7028ACM for hollow bar-feed CNC spindles?
Its ISO 10 light cross-section combines a wide 140 mm through-bore with a compact 210 mm OD and 33 mm width (only 4.14 kg), maximizing bar-pass capacity inside compact headstock castings while the 25° contact angle keeps high-speed axial and radial stiffness tight.
What bearing arrangement works best for 7028ACM inside a large rotary union or lathe headstock?
Single-row angular contact bearings carry axial force in one direction only. Rotary unions typically install a matched DB back-to-back pair to hold pressurized end-thrust and moment loads cleanly, while heavy turning spindles frequently run a triplex DBD stack facing the chuck.
Why is shaft and housing cylindricity especially critical when mounting 7028ACM?
Because the 70-series ring wall is relatively slender (35 mm radial section on a 140 mm bore), out-of-round shaft journals or distorted housing bores transfer directly into raceway geometry, causing erratic preload heat and vibration. Hold precision cylindricity plus da ≥ 150 mm, Da ≤ 200 mm, and fillet below r min = 2.0 mm.
Can ZQM supply 7028ACM in elevated precision grades like P6 or P5 for spindle rebuilds?
Yes—state your required accuracy class (standard P0, P6, or P5), DB/DBD pairing, and preload or clearance target at quotation stage so our factory confirms production lead time, runout test targets, and matched serialization upfront.